

Starting an alcohol production business involves more than purchasing a still. Poor equipment selection, unsuitable production capacity, and inefficient process connections can increase operating costs and delay production. Working with experienced distillery plant manufacturers helps you build a system that matches your products, factory space, and long-term business goals.
An alcohol distillation plant is an integrated production facility that uses fermentation, heating, vapor separation, condensation, and storage equipment to produce beverage spirits such as whisky, vodka, gin, rum, and brandy. A suitable plant combines pot stills, column stills, condensers, fermentation tanks, storage vessels, cooling systems, and process controls according to production capacity and product requirements.
기사 개요
- What Is an Alcohol Distillation Plant and How Does It Work?
- How Do Raw Materials and Fermentation Affect Distillery Plant Design?
- What Types of Distillation Equipment Do Modern Distilleries Need?
- How Do You Choose the Right Distillation System for Different Spirits?
- How Should You Plan Distillery Plant Capacity and Production Efficiency?
- Why Are Heating, Cooling, and Heat Exchangers Important?
- What Materials and Safety Features Should a Distillery Plant Include?
- How Does Automation Improve Alcohol Production?
- What Should a Complete Turnkey Distillery Plant Include?
- How Do You Select the Right Alcohol Distillation Plant Manufacturer?
1. What Is an Alcohol Distillation Plant and How Does It Work?
An alcohol distillation plant is a facility designed to produce concentrated alcoholic spirits from fermented raw materials. It combines several production stages, including raw material preparation, fermentation, distillation, condensation, purification, storage, and packaging.
The main purpose of distillation is to separate alcohol and other volatile components from a fermented liquid. The process uses differences in volatility and boiling behavior to achieve the required alcohol concentration and product characteristics. A distiller can adjust the equipment configuration according to the type of spirit being produced.
A typical beverage distillery plant includes:
| 장비 | Main Function |
|---|---|
| Raw material preparation system | Prepares grain, fruit, or other feedstock |
| Mash cooker | Supports preparation of grain-based materials |
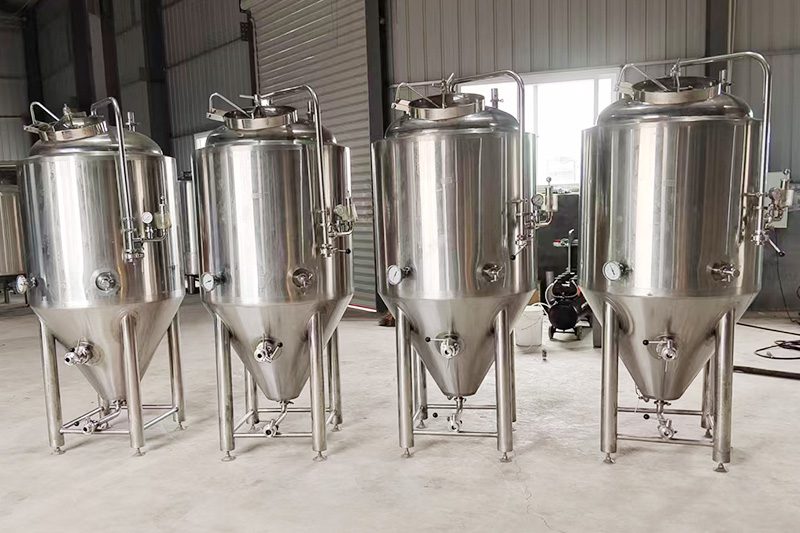
| Fermentation tanks | Convert fermentable sugars into alcohol |
| 포트 스틸 | Supports traditional batch distillation |
| Distillation column | Supports controlled separation and rectification |
| 냉각기 | Converts alcohol vapor into liquid |
| Spirit collection tank | Collects distilled liquid |
| Storage and blending tanks | Hold and prepare finished spirits |
| CIP 시스템 | Supports equipment cleaning |
| Control panel | Monitors and controls production parameters |
The process begins with raw material preparation and fermentation. After fermentation, the liquid moves to the distillation unit, where controlled heating creates vapor. The condenser then cools the vapor into liquid spirit.
For commercial producers, every stage must work together. A well-designed distillation system improves process stability, product consistency, and production efficiency.
2. How Do Raw Materials and Fermentation Affect Distillery Plant Design?
Raw materials play an important role in determining the design of a distillery. Different materials require different preparation methods, fermentation conditions, and equipment configurations.
Common feedstock options include:
- Grains: Barley, wheat, corn, and other cereal grains are used in grain-based spirits.
- Molasses: Commonly used in rum production.
- Fruit: Used for fruit brandy and other specialty spirits.
- Malt: Important for whisky and malt spirit production.
- Sugar-based materials: Used in selected fermentation processes.
The preparation system should match the selected raw materials. For example, a grain-based distillery may need grain handling, milling, mashing, and wort or mash preparation equipment. A rum production line may require equipment suitable for handling molasses and sugar-based fermentation materials.
Why Is Fermentation Capacity Important?
Fermentation determines how much alcohol-containing liquid is available for the next production stage. If fermentation tanks cannot supply enough liquid, the distillation equipment may remain idle.
A commercial distillery should consider:
- Fermentation batch volume.
- Fermentation cycle time.
- Number of fermentation tanks.
- Raw material supply.
- Required alcohol concentration before distillation.
- Distillation schedule.
A professional manufacturer should calculate the relationship between fermentation capacity and still capacity rather than selecting each machine separately.
For example, a whisky producer may require several fermentation tanks to maintain a regular supply of fermented wash. A vodka producer targeting high-purity neutral alcohol may need a different fermentation and rectification arrangement.
MICET provides customized fermentation tanks and distillery equipment for different beverage production requirements.
3. What Types of Distillation Equipment Do Modern Distilleries Need?
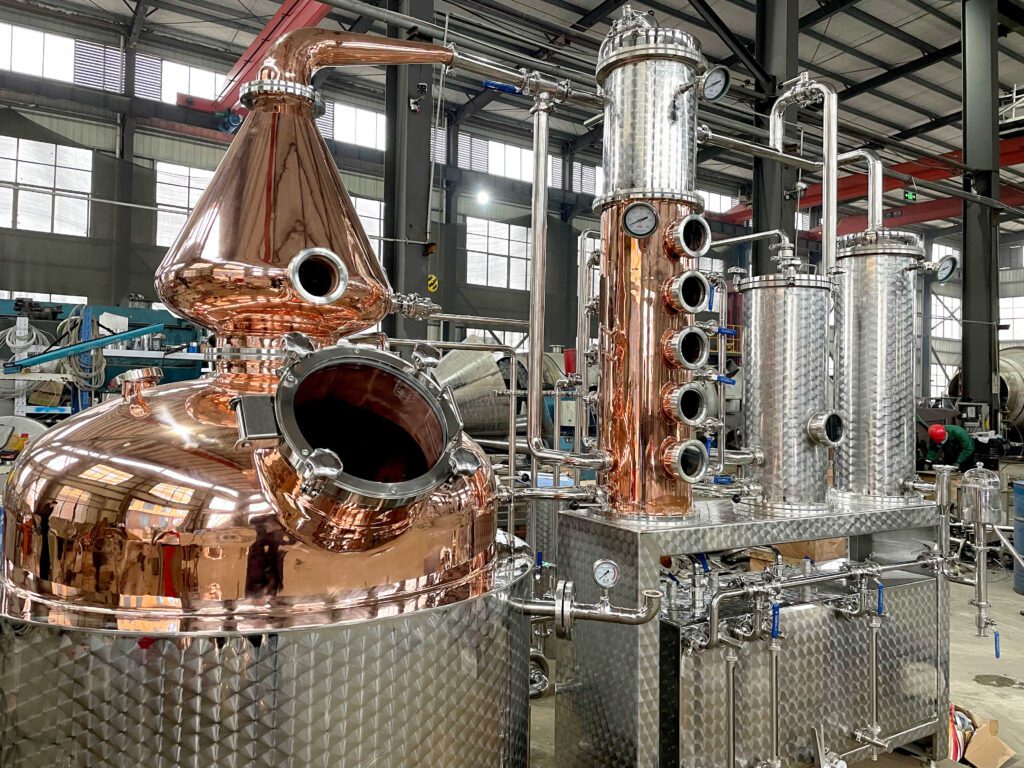
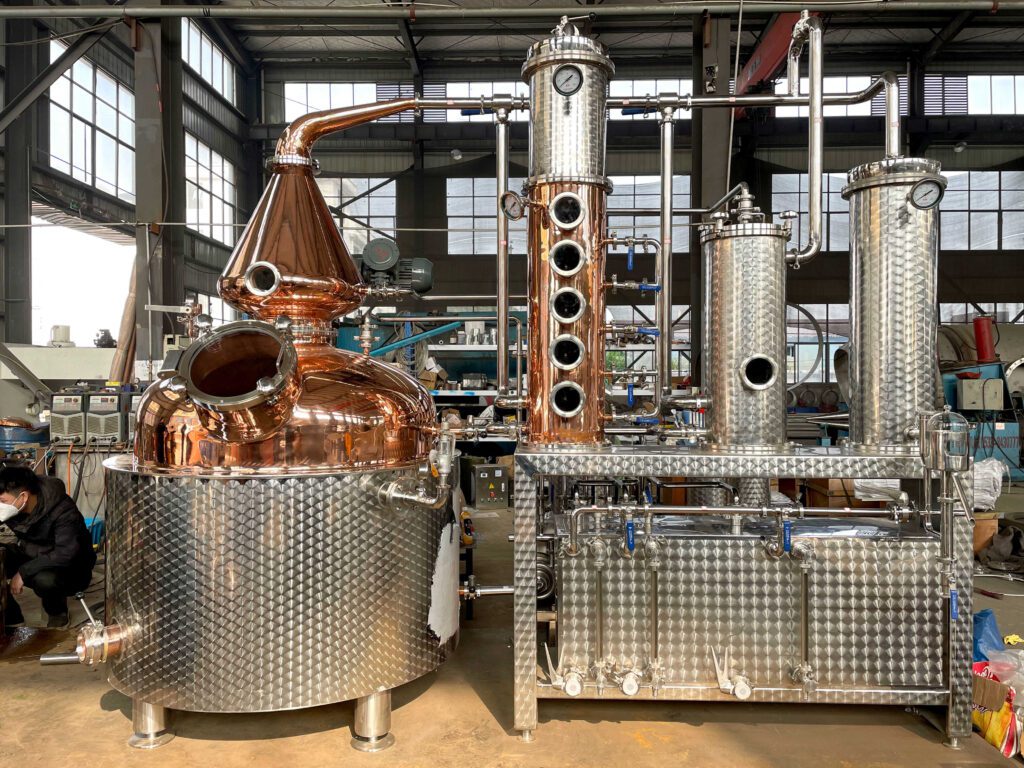
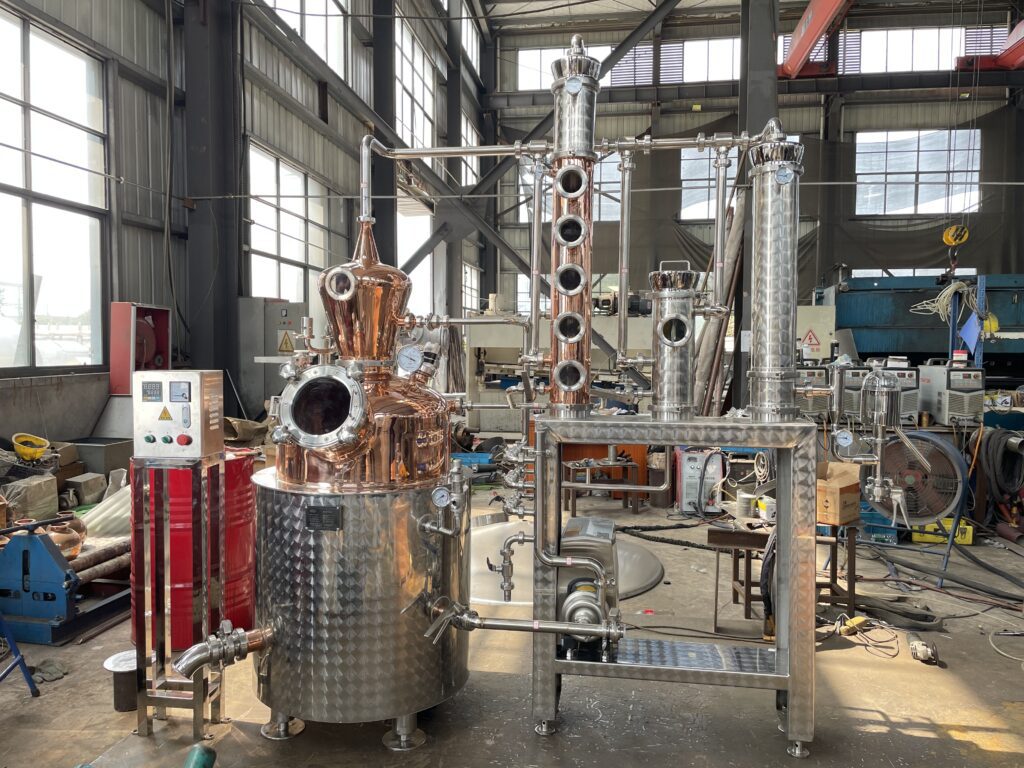
Different distillation plants use different equipment depending on production scale, spirit type, and operating method. The three main still configurations are pot stills, column stills, and hybrid stills.
Pot Still Systems
Best suited for traditional batch spirit production.
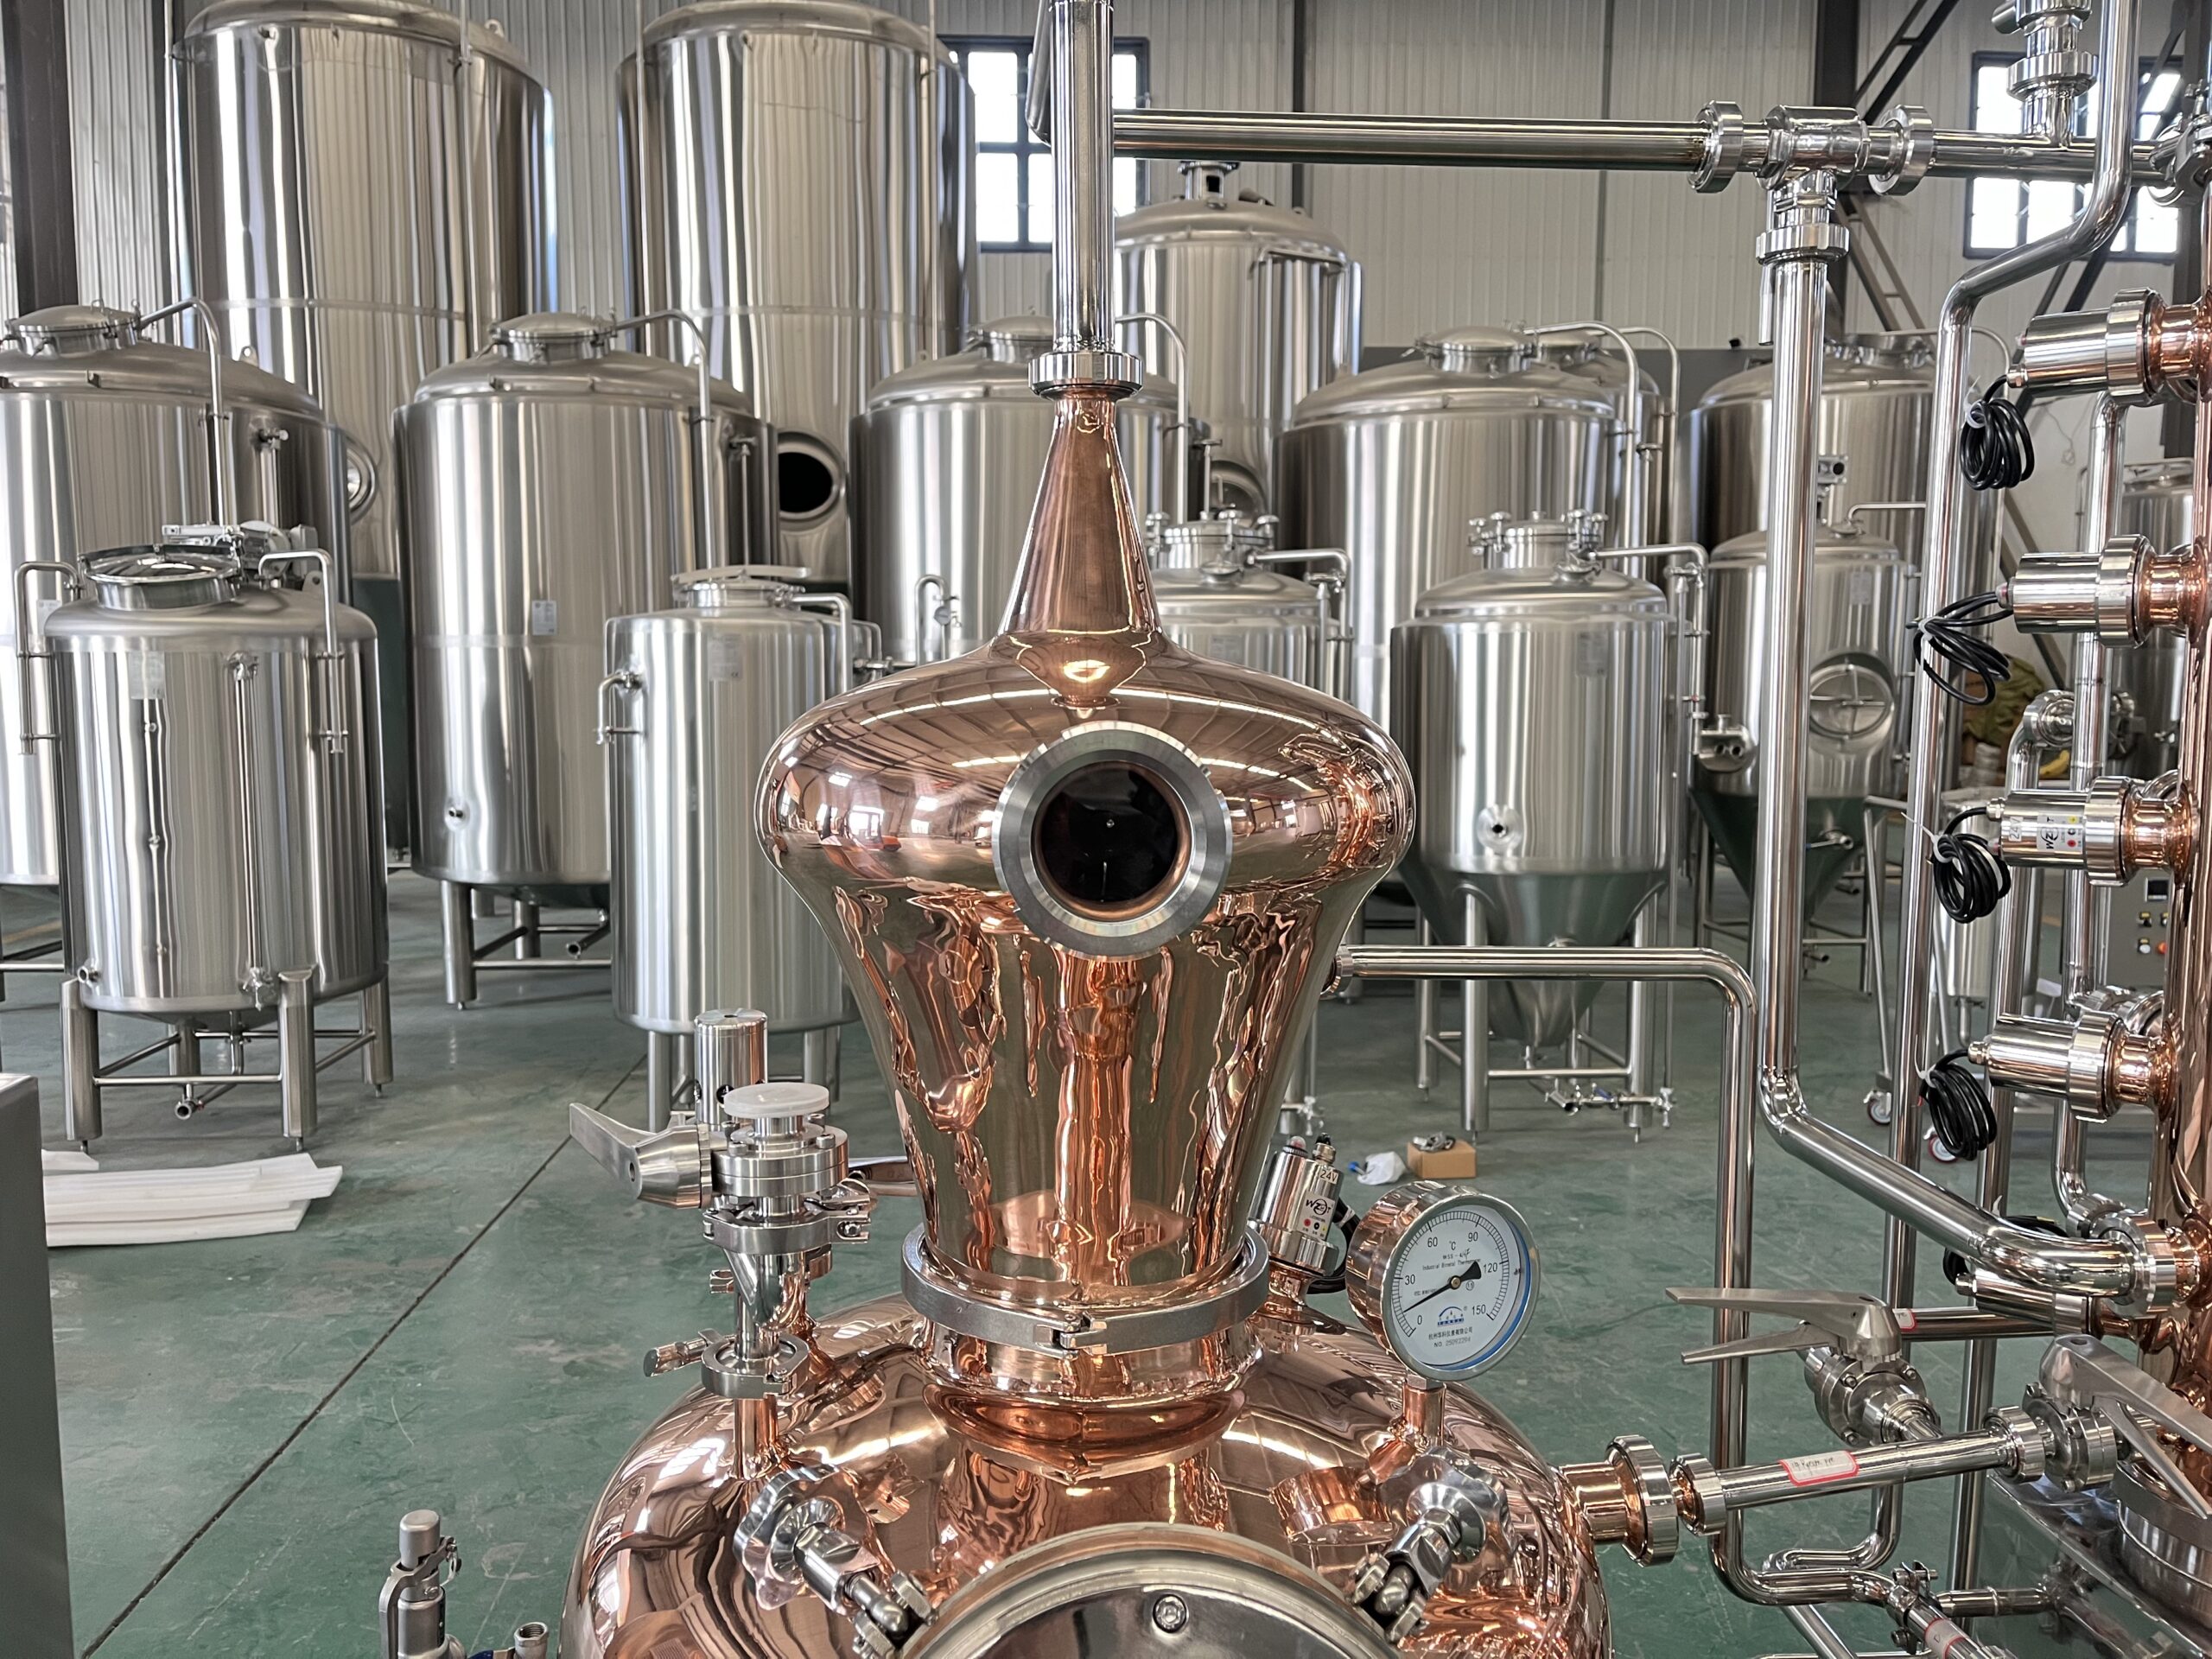
Pot stills are widely used for whisky, rum, brandy, and other flavor-focused spirits. They allow distillers to manage individual batches and adjust production conditions according to the recipe.
A typical pot still system includes:
- Distillation pot
- Heating system
- Still head or copper helmet
- Vapor pipe
- 냉각기
- Spirit collection equipment
Copper components are commonly selected for traditional spirit production because copper interacts with certain sulfur compounds during distillation.
Column Still Systems
Best suited for controlled separation and higher throughput.
A column still uses multiple separation stages to control vapor and liquid contact. The number and arrangement of plates or sections influence the separation performance.
Column systems are commonly used for vodka and neutral spirit production. They can also be configured for other applications that require specific separation characteristics.
Hybrid Still Systems
Best suited for producers making several spirit styles.
A hybrid still combines features of pot still and column still designs. It gives producers more flexibility when developing multiple products.
| Still Type | Main Advantage | Typical Applications |
|---|---|---|
| 포트 스틸 | Traditional flavor development | Whisky, rum, brandy |
| 열 스틸 | Controlled separation and throughput | Vodka, neutral spirits |
| Hybrid Still | Flexible production | Multi-product distilleries |
MICET manufactures and customizes these three core configurations according to spirit style, batch size, and automation requirements.
4. How Do You Choose the Right Distillation System for Different Spirits?
Choosing a distillation system starts with the final product. A whisky distillery has different equipment requirements from a vodka or gin production facility.
For example, whisky producers often focus on flavor development and copper contact. Vodka producers usually require more extensive separation and purification. Gin producers may need botanical infusion equipment to develop their desired aroma.
The following table provides a general reference:
| Spirit Type | Recommended Equipment | Main Design Consideration |
|---|---|---|
| Whisky | Pot still or hybrid still | Flavor development |
| 보드카 | 열 스틸 | Neutral spirit and purity targets |
| 진 | Pot still with gin basket | Botanical extraction |
| 럼 | Pot still or column still | Fermented molasses or sugar-based wash |
| 브랜디 | 포트 스틸 | Fruit character and aroma |
| Neutral spirit | Column distillation system | Separation and product specifications |
What About High-Purity Neutral Alcohol?
Some producers require extra neutral alcohol (ENA) or other high-purity neutral spirits.
These applications require suitable column configuration, reflux management, product monitoring, and downstream purification where specified. The equipment should be engineered around the required product specification rather than a general claim of high purity.
For vodka manufacturers, MICET offers customized distillation solutions, including a 20-layer copper distillation column and PLC-based process control options.
A professional distiller should discuss the target alcohol strength, throughput, product characteristics, and applicable local requirements before finalizing the system.
5. How Should You Plan Distillery Plant Capacity and Production Efficiency?
Production capacity is one of the most important decisions when planning a new alcohol plant.
A system that is too small may limit business growth. An oversized distillery plant can increase initial investment, utility costs, and unused equipment capacity.
Before selecting a production plant, calculate:
- Expected annual production.
- Required output per batch.
- Number of operating days.
- Fermentation cycle time.
- Distillation cycle time.
- Storage requirements.
- Future expansion plans.
MICET Distillery Equipment Capacity Range
MICET provides distillery equipment configurations across several capacities.
| Equipment Capacity | Typical Project Positioning |
|---|---|
| 200L | Pilot production and small distilleries |
| 300L | Small-scale craft spirit production |
| 500L | Growing craft distilleries |
| 800L | Expanded small commercial production |
| 1,000L | Commercial craft distilleries |
| 1,500L | Growing commercial operations |
| 2,000L | Medium-scale production |
| 3,000L | Larger commercial projects |
| 5,000L | Higher-capacity production facilities |
These capacities represent available equipment configurations, not guaranteed finished alcohol output. Actual production depends on working volume, raw materials, fermentation performance, distillation cycles, and product specifications.
Why Is Future Expansion Important?
A new distillery may start with a relatively small production target. However, successful products can create demand for higher output.
A scalable layout should leave room for:
- Additional fermentation tanks.
- Larger distillation columns.
- Extra storage tanks.
- New filtration equipment.
- Expanded cooling capacity.
- Additional packaging equipment.
This approach helps businesses expand without rebuilding the entire facility.
6. Why Are Heating, Cooling, and Heat Exchangers Important?
Heating and cooling systems have a direct effect on distillation performance.
The heating system provides the energy required to bring fermented liquid to the operating temperature. Steam heating, electric heating, and other suitable heating arrangements can be selected according to project requirements.
A condenser then cools the vapor and converts it into liquid. Its capacity must match the expected vapor load and operating conditions.
Main Utility Systems
| Utility | 목적 | Planning Consideration |
|---|---|---|
| Steam or electric heating | Supplies process heat | Heating capacity and energy source |
| Cooling water | Supports condensation | Water flow and temperature |
| Glycol system | Supports process cooling | Cooling load and temperature |
| Heat exchangers | Transfer heat between process streams | Thermal duty and flow |
| Water supply | Supports production and cleaning | Water quality and availability |
| Compressed air | Operates pneumatic equipment | Pressure and consumption |
How Can Heat Recovery Improve Energy Efficiency?
Heat exchangers can transfer heat from one process stream to another. For example, recovered heat may support preheating of incoming process liquid when the system is designed for this purpose.
This can reduce the amount of additional heating energy required.
However, the actual benefit depends on temperature differences, flow rates, operating schedules, and equipment design.
An industrial distillation plant should consider heating and cooling as one integrated system rather than treating them as separate accessories.
For international projects, utility design should also account for local electricity supply, steam availability, water conditions, and installation requirements.
7. What Materials and Safety Features Should a Distillery Plant Include?
Material selection affects sanitation, durability, maintenance, and product quality.
Stainless steel is widely used in fermentation tanks, storage tanks, process piping, and other product-contact equipment. Copper is also important in traditional spirit production.
A well-designed system may combine the two materials according to the intended application.
Stainless Steel vs. Copper
| 재료 | Advantages | Common Applications |
|---|---|---|
| Stainless Steel | Corrosion resistance, hygienic surface, easy cleaning | Tanks, pipes, storage vessels |
| 구리 | Traditional distillation material and interaction with sulfur compounds | Still heads, columns, vapor-contact components |
The selected grade, thickness, surface finish, welding quality, and cleaning design should be documented in the technical specification.
What Safety Features Should Plant Manufacturers Provide?
Alcohol vapor is flammable. Therefore, safety engineering must be part of the original plant design.
Important considerations include:
- Suitable ventilation.
- Electrical equipment appropriate for the classified area.
- Pressure protection.
- Temperature monitoring.
- Emergency shutdown arrangements.
- Proper grounding and bonding.
- Safe vapor handling.
- Suitable pipework and valves.
- Operator training and maintenance procedures.
Equipment manufacturers should coordinate their design with local engineering and compliance professionals. Equipment supply alone does not replace local permits or site approvals.
8. How Does Automation Improve Alcohol Production?
Modern distilleries need stable process control to maintain consistent product quality.
Manual operation may be suitable for some small batch systems. However, growing facilities often benefit from PLC automation and digital monitoring.
A process control system can monitor:
- Heating temperature.
- Pressure.
- Liquid levels.
- Flow rates.
- Cooling conditions.
- Pump operation.
- Valve status.
- Production alarms.
Automation can help reduce operator workload and improve production repeatability.
Basic vs. Advanced Automation
| Feature | Basic Control | Advanced PLC Control |
|---|---|---|
| Temperature monitoring | Manual or digital display | Integrated sensors |
| Heating control | Operator adjustment | Automatic control |
| Valve operation | Manual | Automatic or pneumatic |
| Process monitoring | Local instruments | Central control panel |
| Alarm functions | Limited | Configurable alarms |
| Production records | Manual | Optional digital records |
Not every distillery needs a fully automated production line.
A small craft distiller may prefer a simple control panel with essential temperature and safety functions. A larger commercial facility may benefit from integrated controls across fermentation, heating, cooling, and distillation.
MICET can configure control options according to the actual process, equipment arrangement, and operator requirements.
9. What Should a Complete Turnkey Distillery Plant Include?
A turnkey distillery project should cover more than the main still.
It should connect raw material preparation, fermentation, distillation, storage, cleaning, and packaging into one practical production layout.
A typical project may include:
| Production Section | 주요 장비 |
|---|---|
| Raw Material Handling | Grain handling, milling, transfer equipment |
| Mash Preparation | Mash tun, mash cooker, heating system |
| 발효 | Stainless steel fermentation tanks |
| Primary Distillation | Pot still or hybrid still |
| Rectification | Column still and related components |
| 응축 | Condenser and cooling system |
| 스토리지 | Spirit storage tanks |
| Blending | Blending tanks and transfer pumps |
| 청소 | CIP 시스템 |
| 포장 | Bottle filling and packaging equipment |
| 자동화 | PLC, sensors, valves, and control panels |
A complete project also requires layout planning, utility connections, transportation, installation guidance, testing, and operator training.
How Does a Manufacturer Support the Whole Project?
Working with one experienced manufacturer can simplify coordination between different equipment groups.
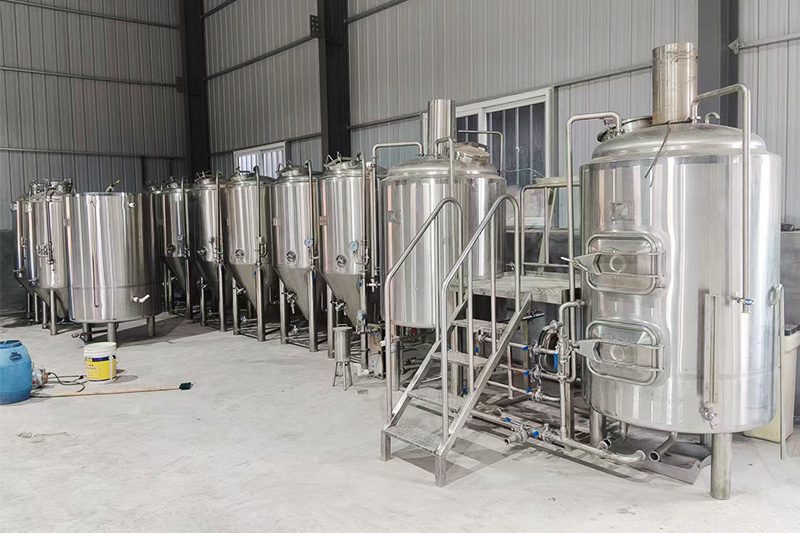
As a professional brewery, distillery, and beverage equipment manufacturing plant, MICET provides customized stainless steel brewing systems, fermentation tanks, brewhouse systems, and distillery solutions for global B2B customers.
Our project support focuses on:
- Customized equipment configuration.
- Production capacity planning.
- Equipment layout and integration.
- Stainless steel and copper fabrication.
- Process and utility coordination.
- Equipment inspection and testing.
- Installation and commissioning guidance.
- Long-term technical support.
We can also evaluate hybrid new-and-used equipment packages where suitable, helping customers manage initial investment while maintaining important safety and process requirements.
10. How Do You Select the Right Alcohol Distillation Plant Manufacturer?
Choosing between alcohol distillation plant manufacturers should involve more than comparing the best price.
A suitable manufacturer needs to understand your intended spirits, production capacity, site conditions, equipment configuration, and long-term operating goals.
Use the following checklist when evaluating a potential supplier:
| Evaluation Factor | What Buyers Should Confirm |
|---|---|
| Manufacturing capability | Factory production and fabrication experience |
| Process knowledge | Experience with the intended spirit type |
| 사용자 지정 | Capacity, still type, and layout options |
| 자료 | Stainless steel and copper specifications |
| Process integration | Fermentation, distillation, storage, and cooling |
| Safety | Pressure protection and electrical requirements |
| 자동화 | PLC, temperature, and process monitoring |
| Quality control | Inspection and testing documentation |
| Export experience | Packing, shipping, and technical documents |
| After-sales service | Installation guidance and spare parts |
What Information Should You Prepare Before Requesting a Quote?
To help the manufacturer prepare a suitable proposal, provide:
- Spirit type: whisky, gin, vodka, rum, brandy, or other products.
- Target production capacity: liters per batch or annual output.
- Preferred still type: pot, column, or hybrid.
- Raw materials and fermentation requirements.
- Available factory dimensions.
- Heating source and utility conditions.
- Automation requirements.
- Destination country and applicable standards.
- Project budget and expected delivery schedule.
MICET is a manufacturer and exporter of customized brewery, distillery, and beverage equipment. Our team can help develop a suitable plant configuration based on your production goals, available space, and investment plan.
Whether you are establishing a small craft distillery or expanding a commercial alcohol production facility, the right engineering partner can help reduce project risk and support stable operation.
Contact MICET to discuss your alcohol distillation plant project. Share your target capacity, spirit type, and factory layout to receive a customized equipment proposal.
Frequently Asked Questions
What equipment is required for an alcohol distillation plant?
A typical plant requires raw material preparation equipment, fermentation tanks, pot or column stills, condensers, storage tanks, pumps, piping, cooling systems, and control panels. Additional equipment depends on the spirit type and production capacity.
팟 스틸과 컬럼 스틸의 차이점은 무엇인가요?
A pot still is mainly used for batch distillation and traditional flavor-focused spirits. A column still provides multiple separation stages and is often selected for neutral spirits and higher-throughput production. Hybrid systems combine features of both designs.
How much capacity does a commercial distillery need?
There is no universal capacity. A small craft distillery may begin with a 200L–500L system, while growing commercial producers may consider 1,000L–5,000L configurations. The correct choice depends on production targets, fermentation time, and operating schedules.
Can one distillery produce whisky, gin, vodka, and rum?
Yes, a suitably designed distillery can produce several spirit types. However, different products may require different still configurations, botanical baskets, fermentation arrangements, and cleaning procedures. The system should be designed around the planned product range.
What is the role of a distillation column?
A distillation column provides repeated vapor-liquid contact to support separation of alcohol and other volatile components. Its configuration, number of plates or sections, reflux arrangement, and operating conditions influence separation performance.
Do distillery plant manufacturers provide turnkey solutions?
Many professional manufacturers provide complete project services, including equipment design, manufacturing, layout planning, utility coordination, installation guidance, commissioning support, and technical service. The exact project scope should be confirmed in the quotation.
Key Points to Remember
- An alcohol distillation plant requires coordinated equipment from raw material preparation to finished spirit storage.
- Pot stills, column stills, and hybrid stills serve different production requirements.
- Raw materials and fermentation capacity influence the complete plant configuration.
- Production capacity should match actual demand and future expansion plans.
- Heating, cooling, condensers, and heat exchangers affect energy efficiency.
- Stainless steel and copper have different roles in professional distillery equipment.
- Safety engineering and local compliance must be considered before installation.
- PLC automation can improve process monitoring and production consistency.
- A turnkey distillery solution simplifies equipment integration and project coordination.
- Choosing an experienced manufacturer supports reliable production and long-term business growth.